Food Manufacturing

Food processing heat recovery systems

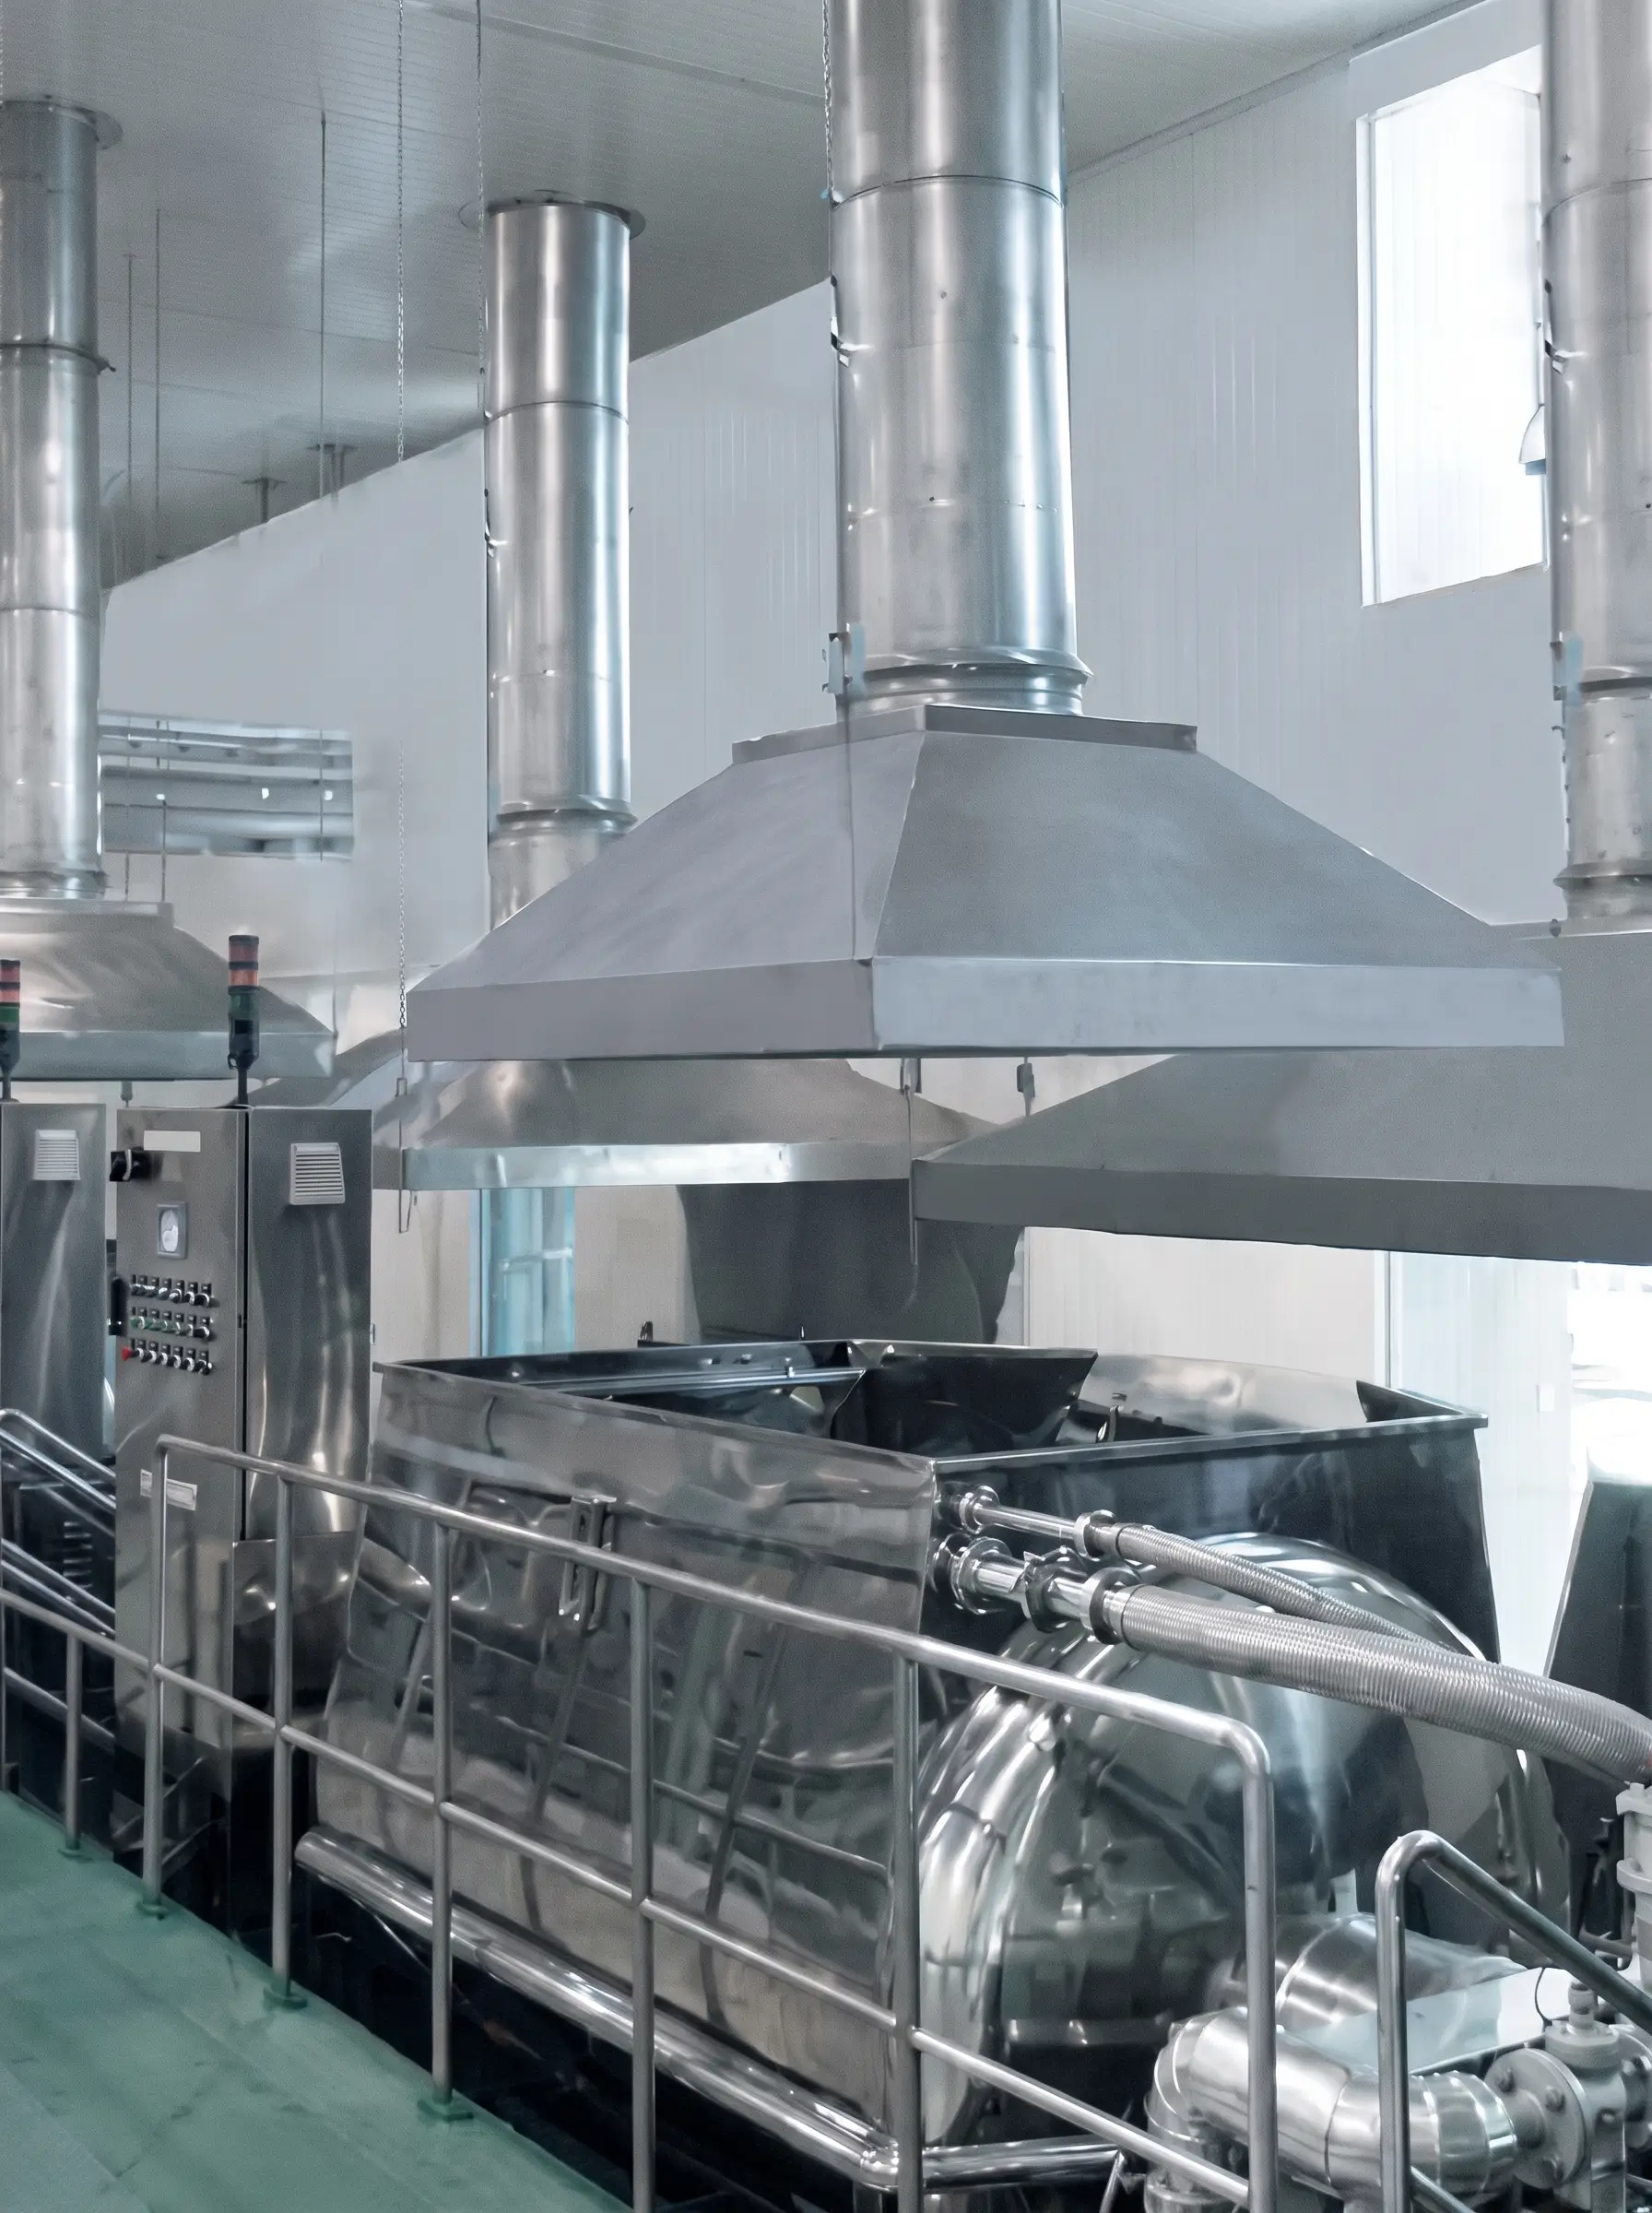
Food processing heat recovery systems can capture energy from ovens, dryers, cook lines, and other heated exhaust. That energy may be reused for process water, boiler feedwater, makeup air, process air, or another approved load. 

WHY FOOD PLANTS ARE HARD

Food manufacturing heat recovery in humid process conditions

The strongest opportunity pairs a reliable source with a demand that operates at the same time.

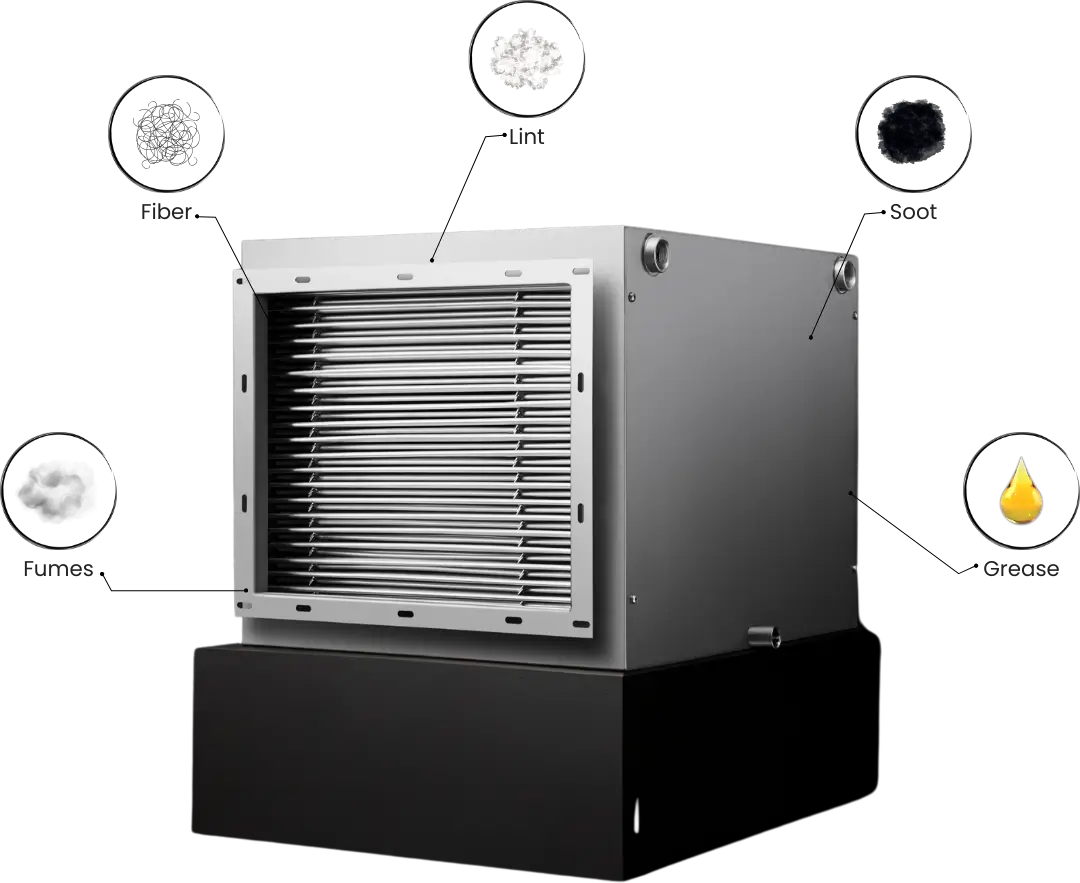
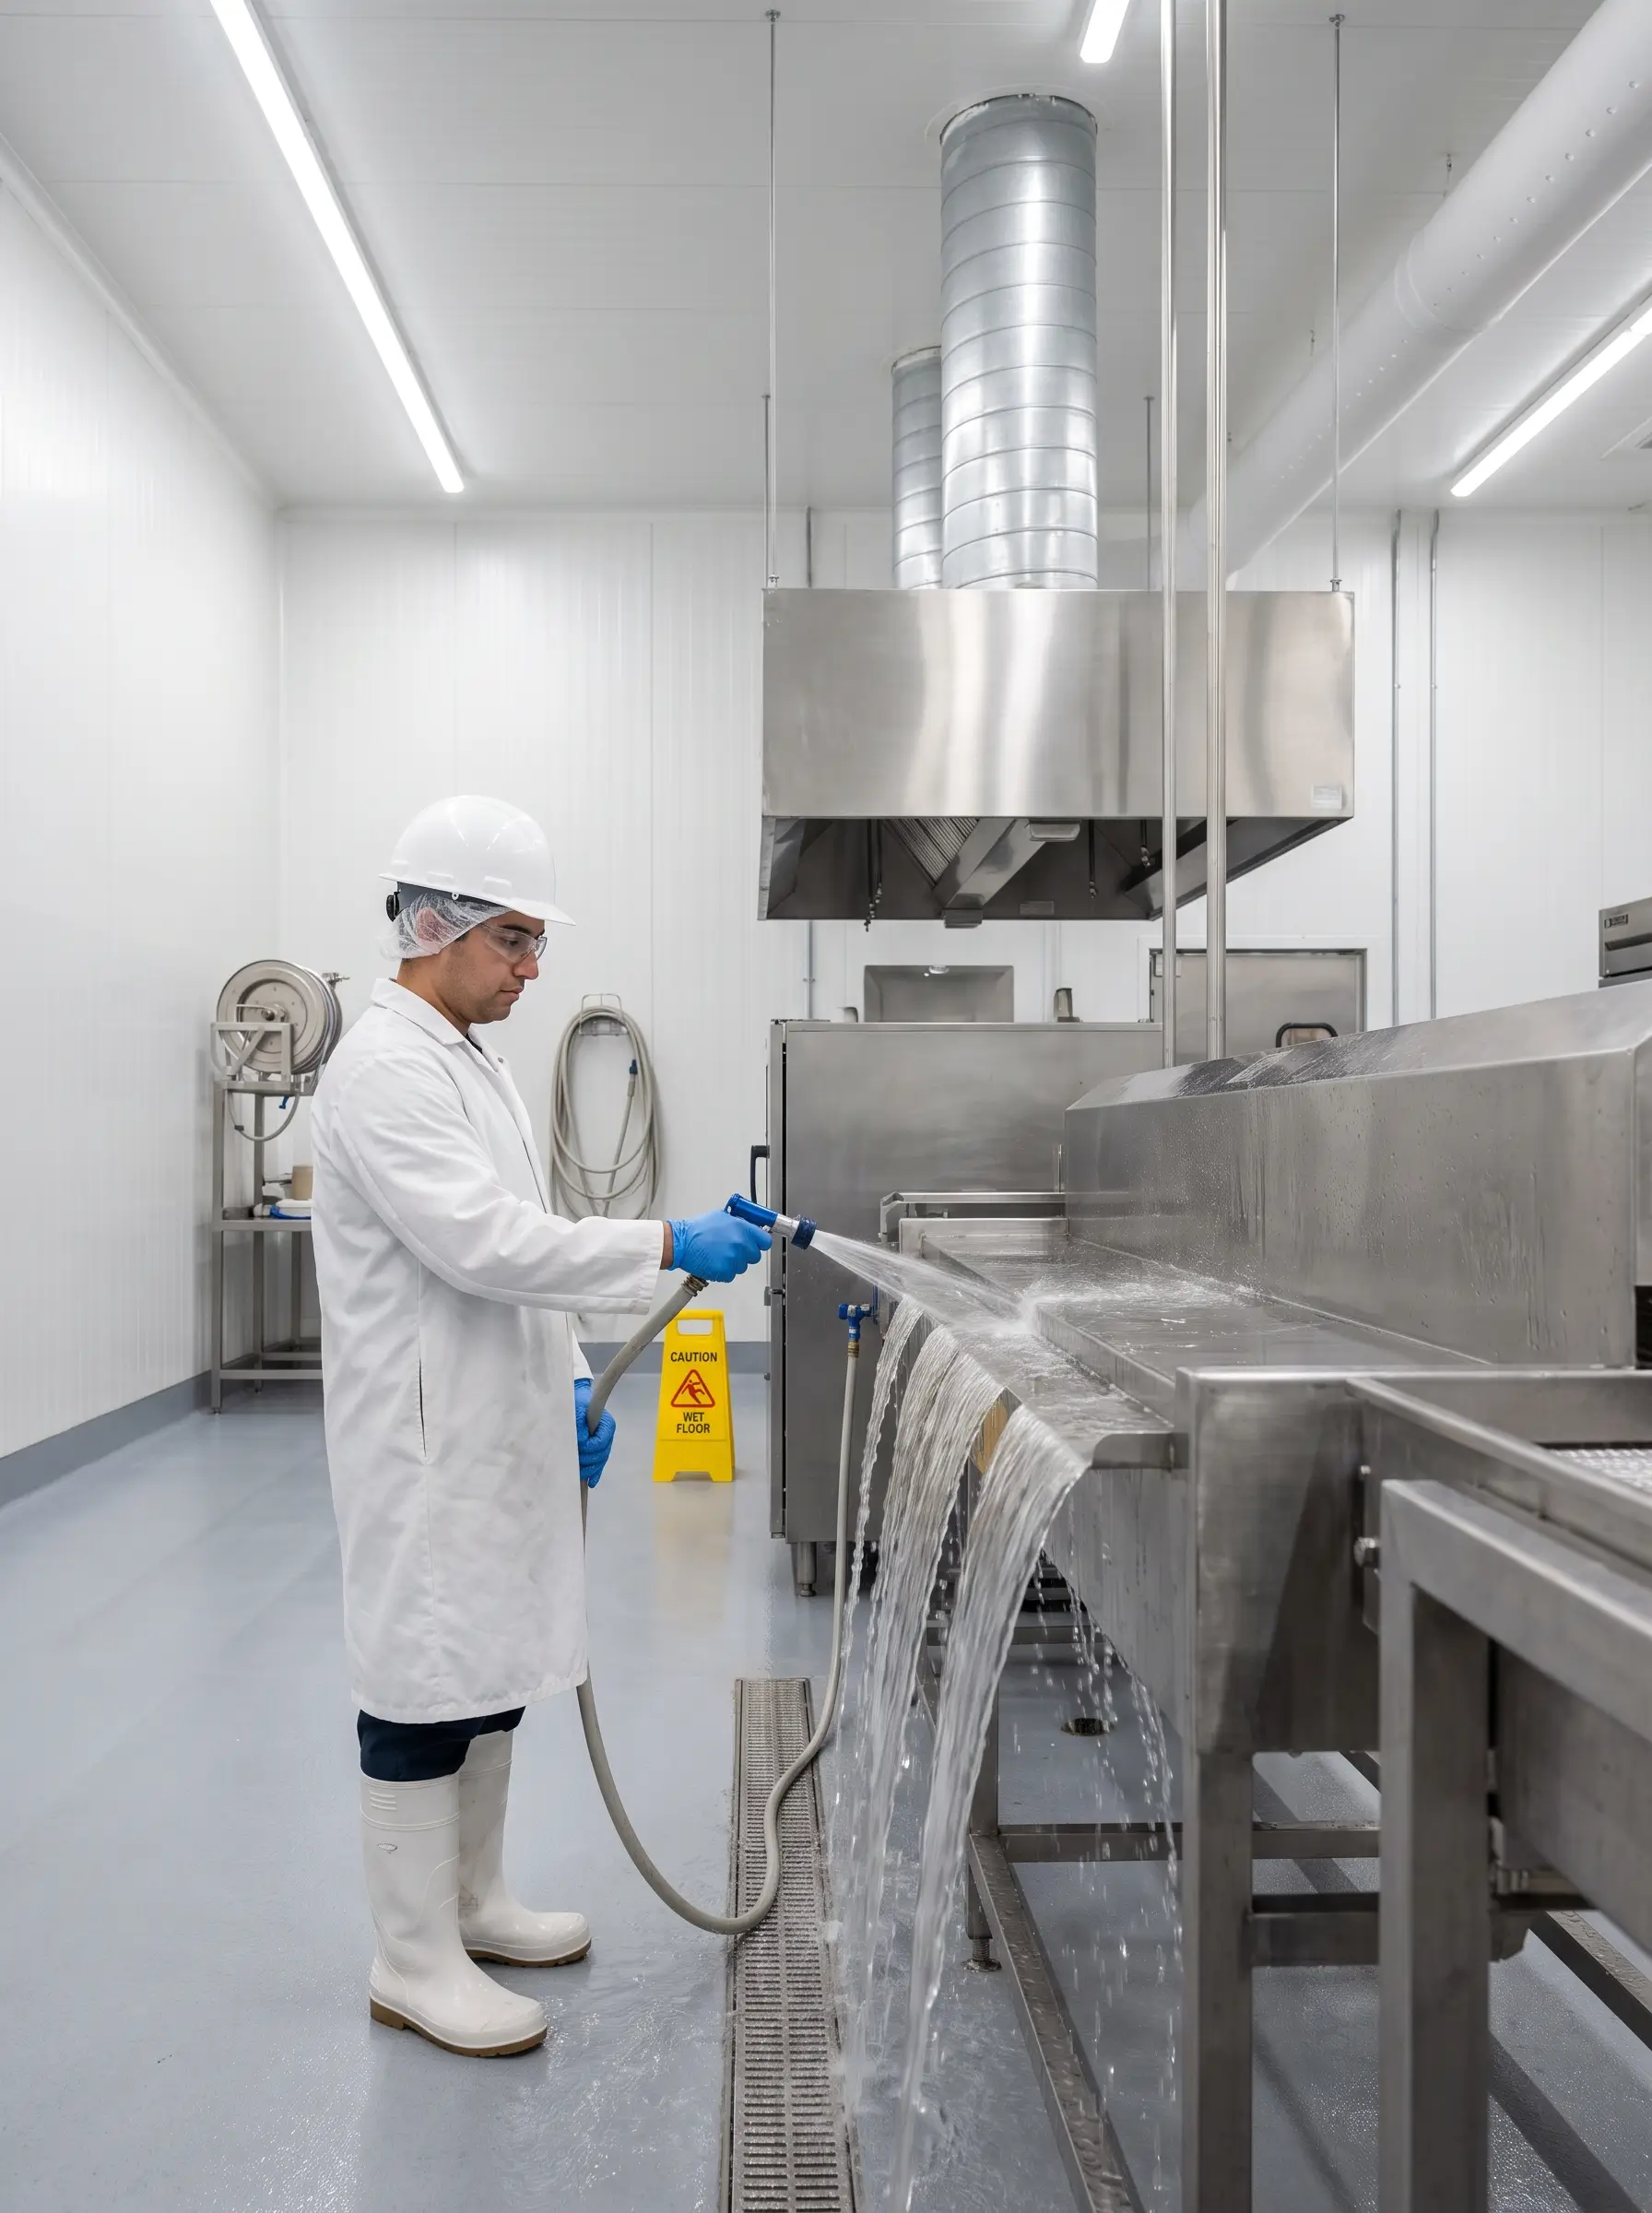
Food manufacturing heat recovery must account for moisture, particles, oils, cleaning practices, sanitation requirements, and production variation. Conventional dense surfaces may accumulate material and become maintenance intensive. Lepido® is designed with open, finless pathways that support particle passage and stable airflow in approved applications.

Contaminants Lepido is designed to handle: lint, grease, dust and moisture
WHERE THE HEAT COMES FROM

Applications across the plant

Food manufacturing waste heat solutions can be configured around one process or evaluated across several lines.

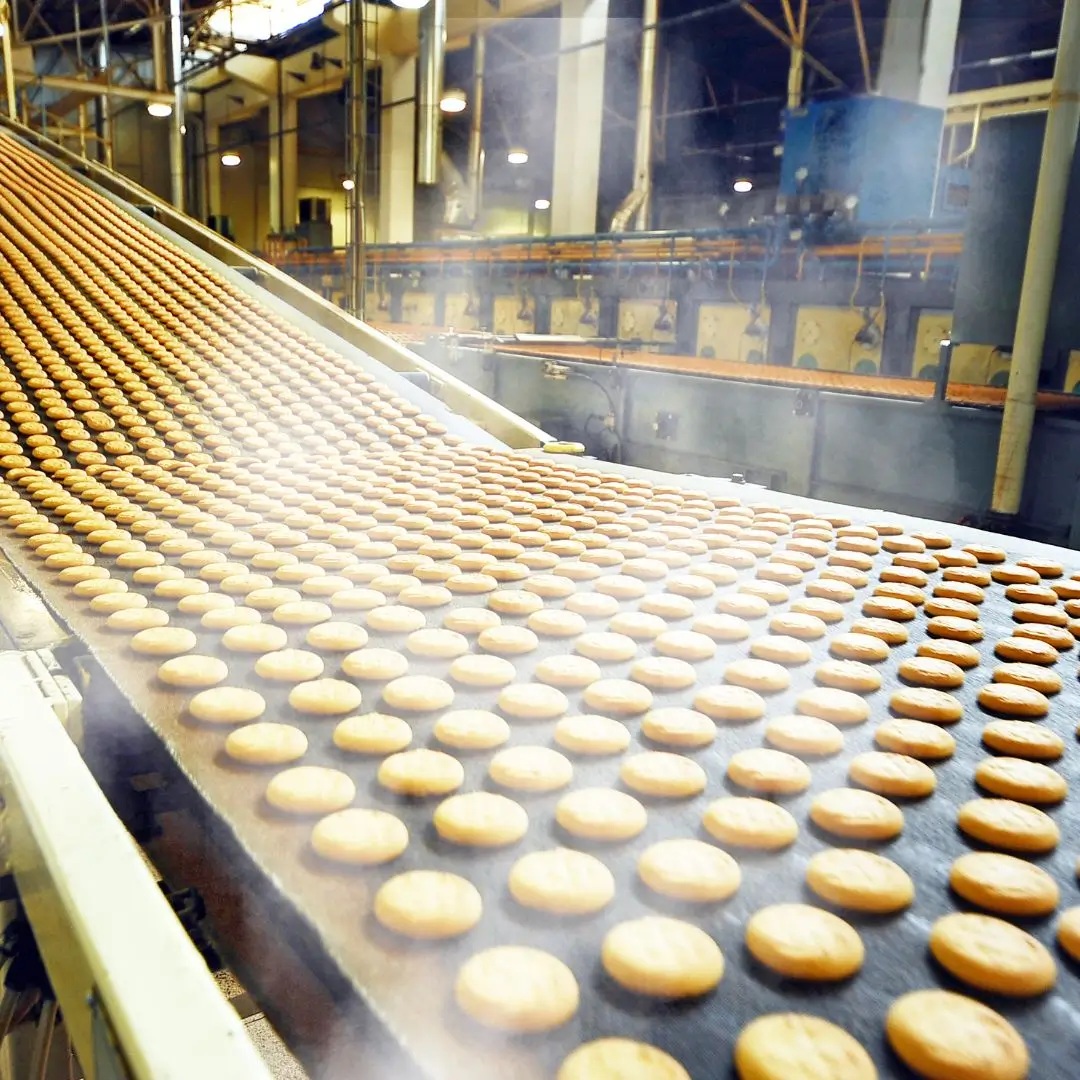
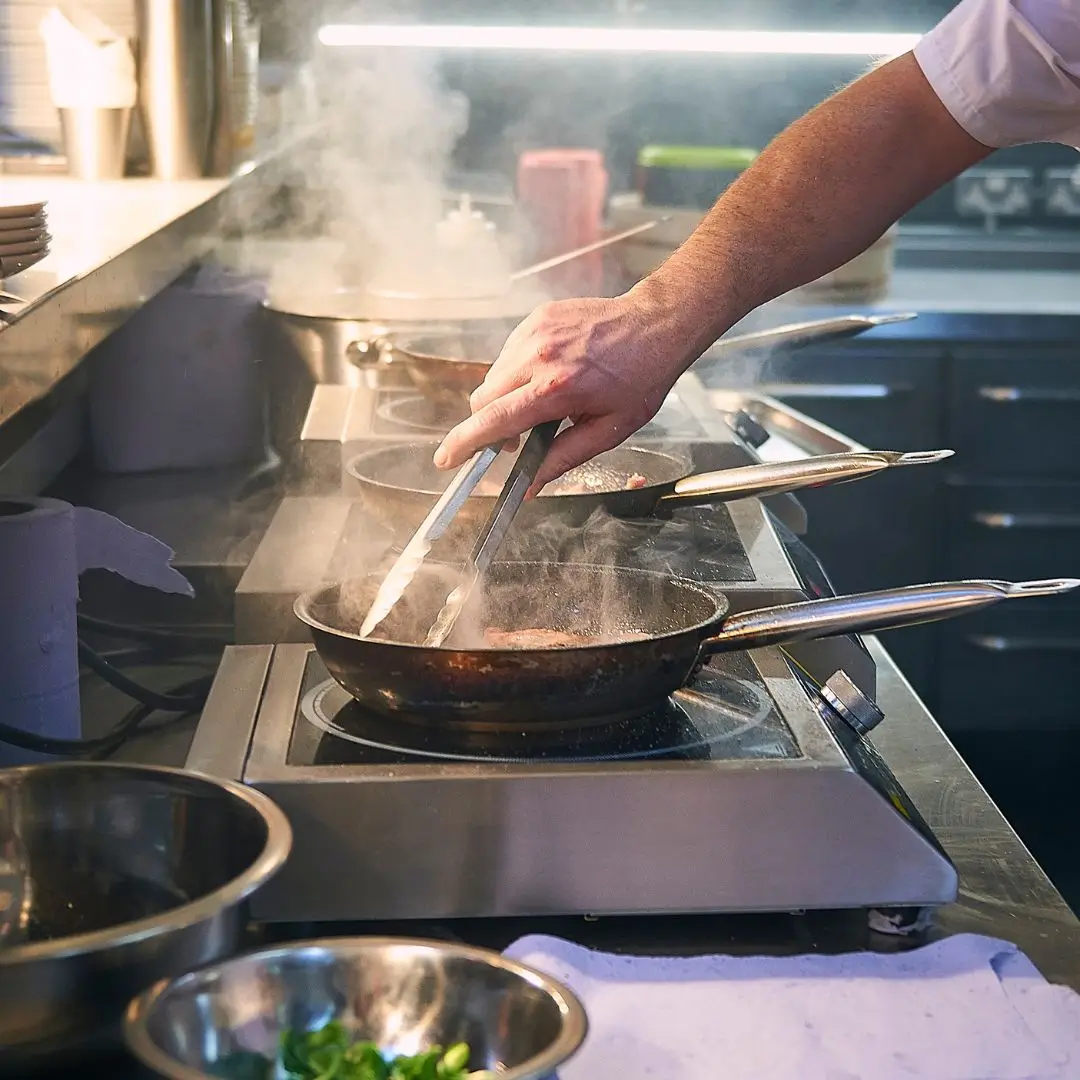
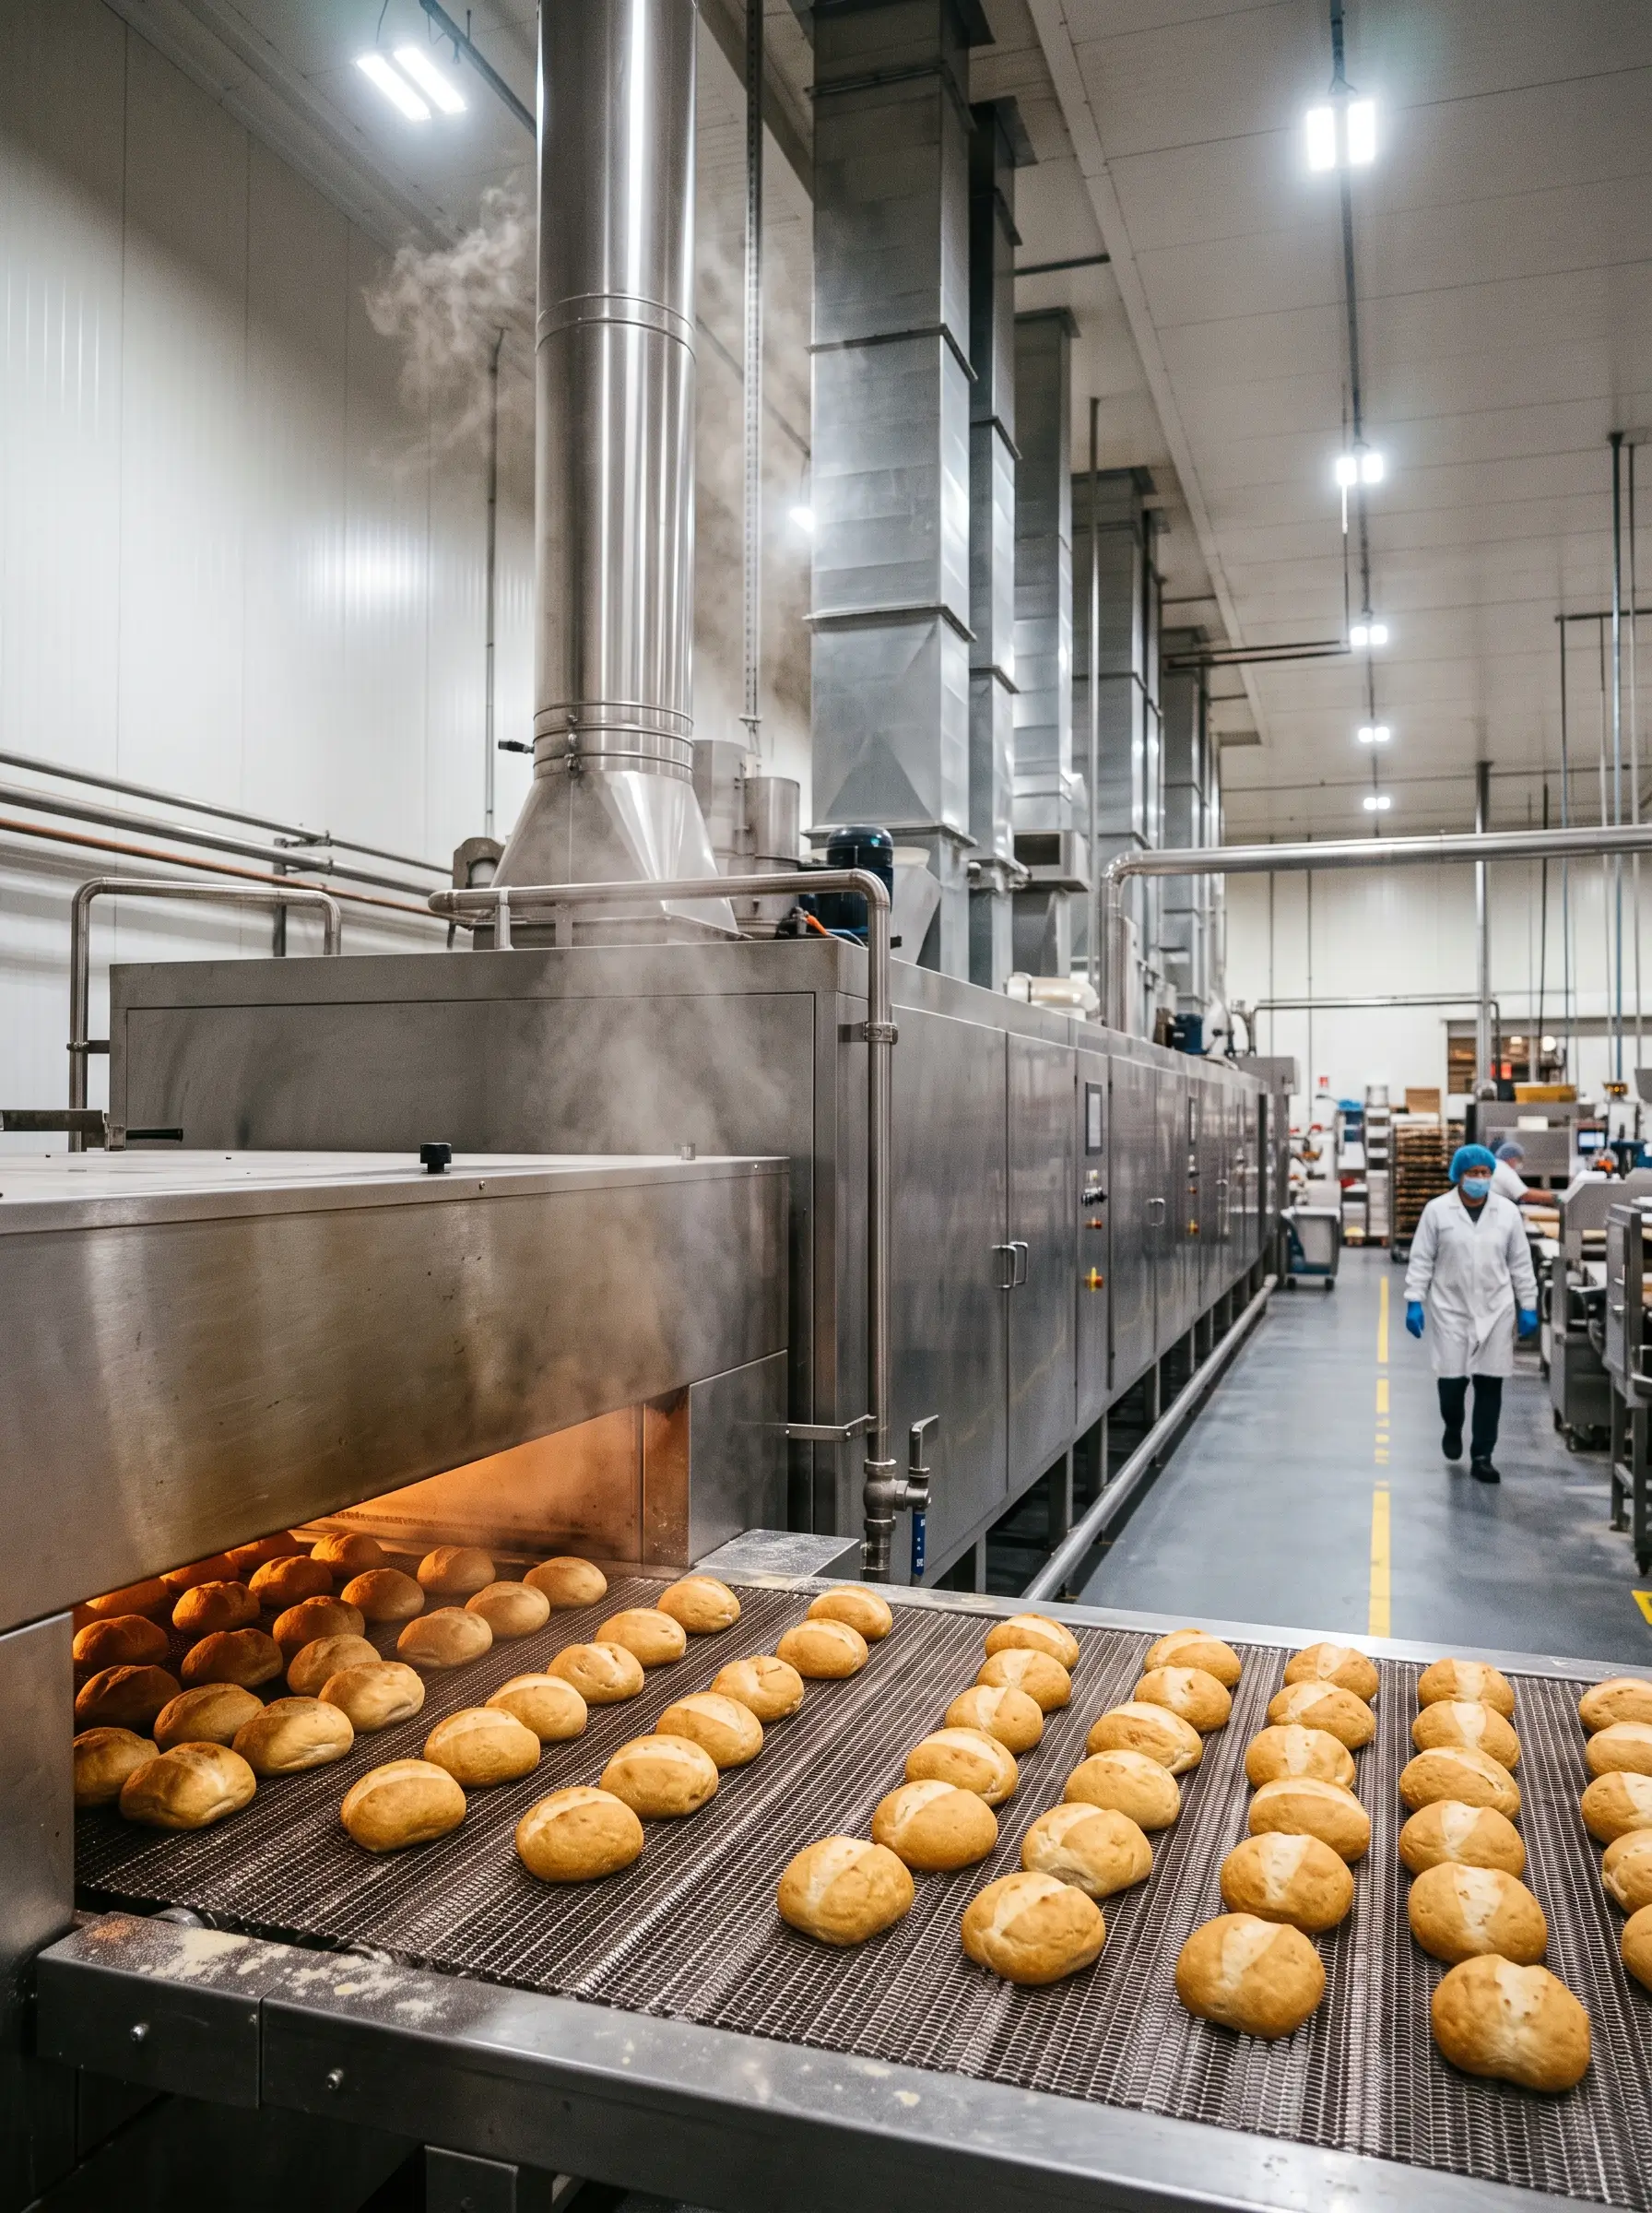
Bakery exhaust heat recovery may capture energy from ovens, while other facilities may evaluate dryers, roasters, fryers, or process ventilation. Every source requires application specific review before equipment is selected.

Bread rolls leaving a tunnel oven in a food plant
HEAT DELIVERED, NOT STACK TEMPERATURE

Economic and operating value

Food manufacturing energy savings depend on the amount of useful heat delivered, not only the temperature at the stack. ThermStar compares source capacity with the receiving load and operating schedule. Energy rates, production hours, existing equipment, integration, maintenance, and incentives all affect the project case.

PRODUCTION COMES FIRST

Support plant priorities

Food plant energy efficiency projects must respect production, product quality, sanitation, safety, and maintenance requirements. ThermStar supplies heat recovery components, systems, technology, and related support. The customer and its qualified engineering and installation partners retain responsibility for their project scopes and facility requirements.
Economic and operating value
Support plant priorities
TWO THINGS TO SEND

Assess a source and demand

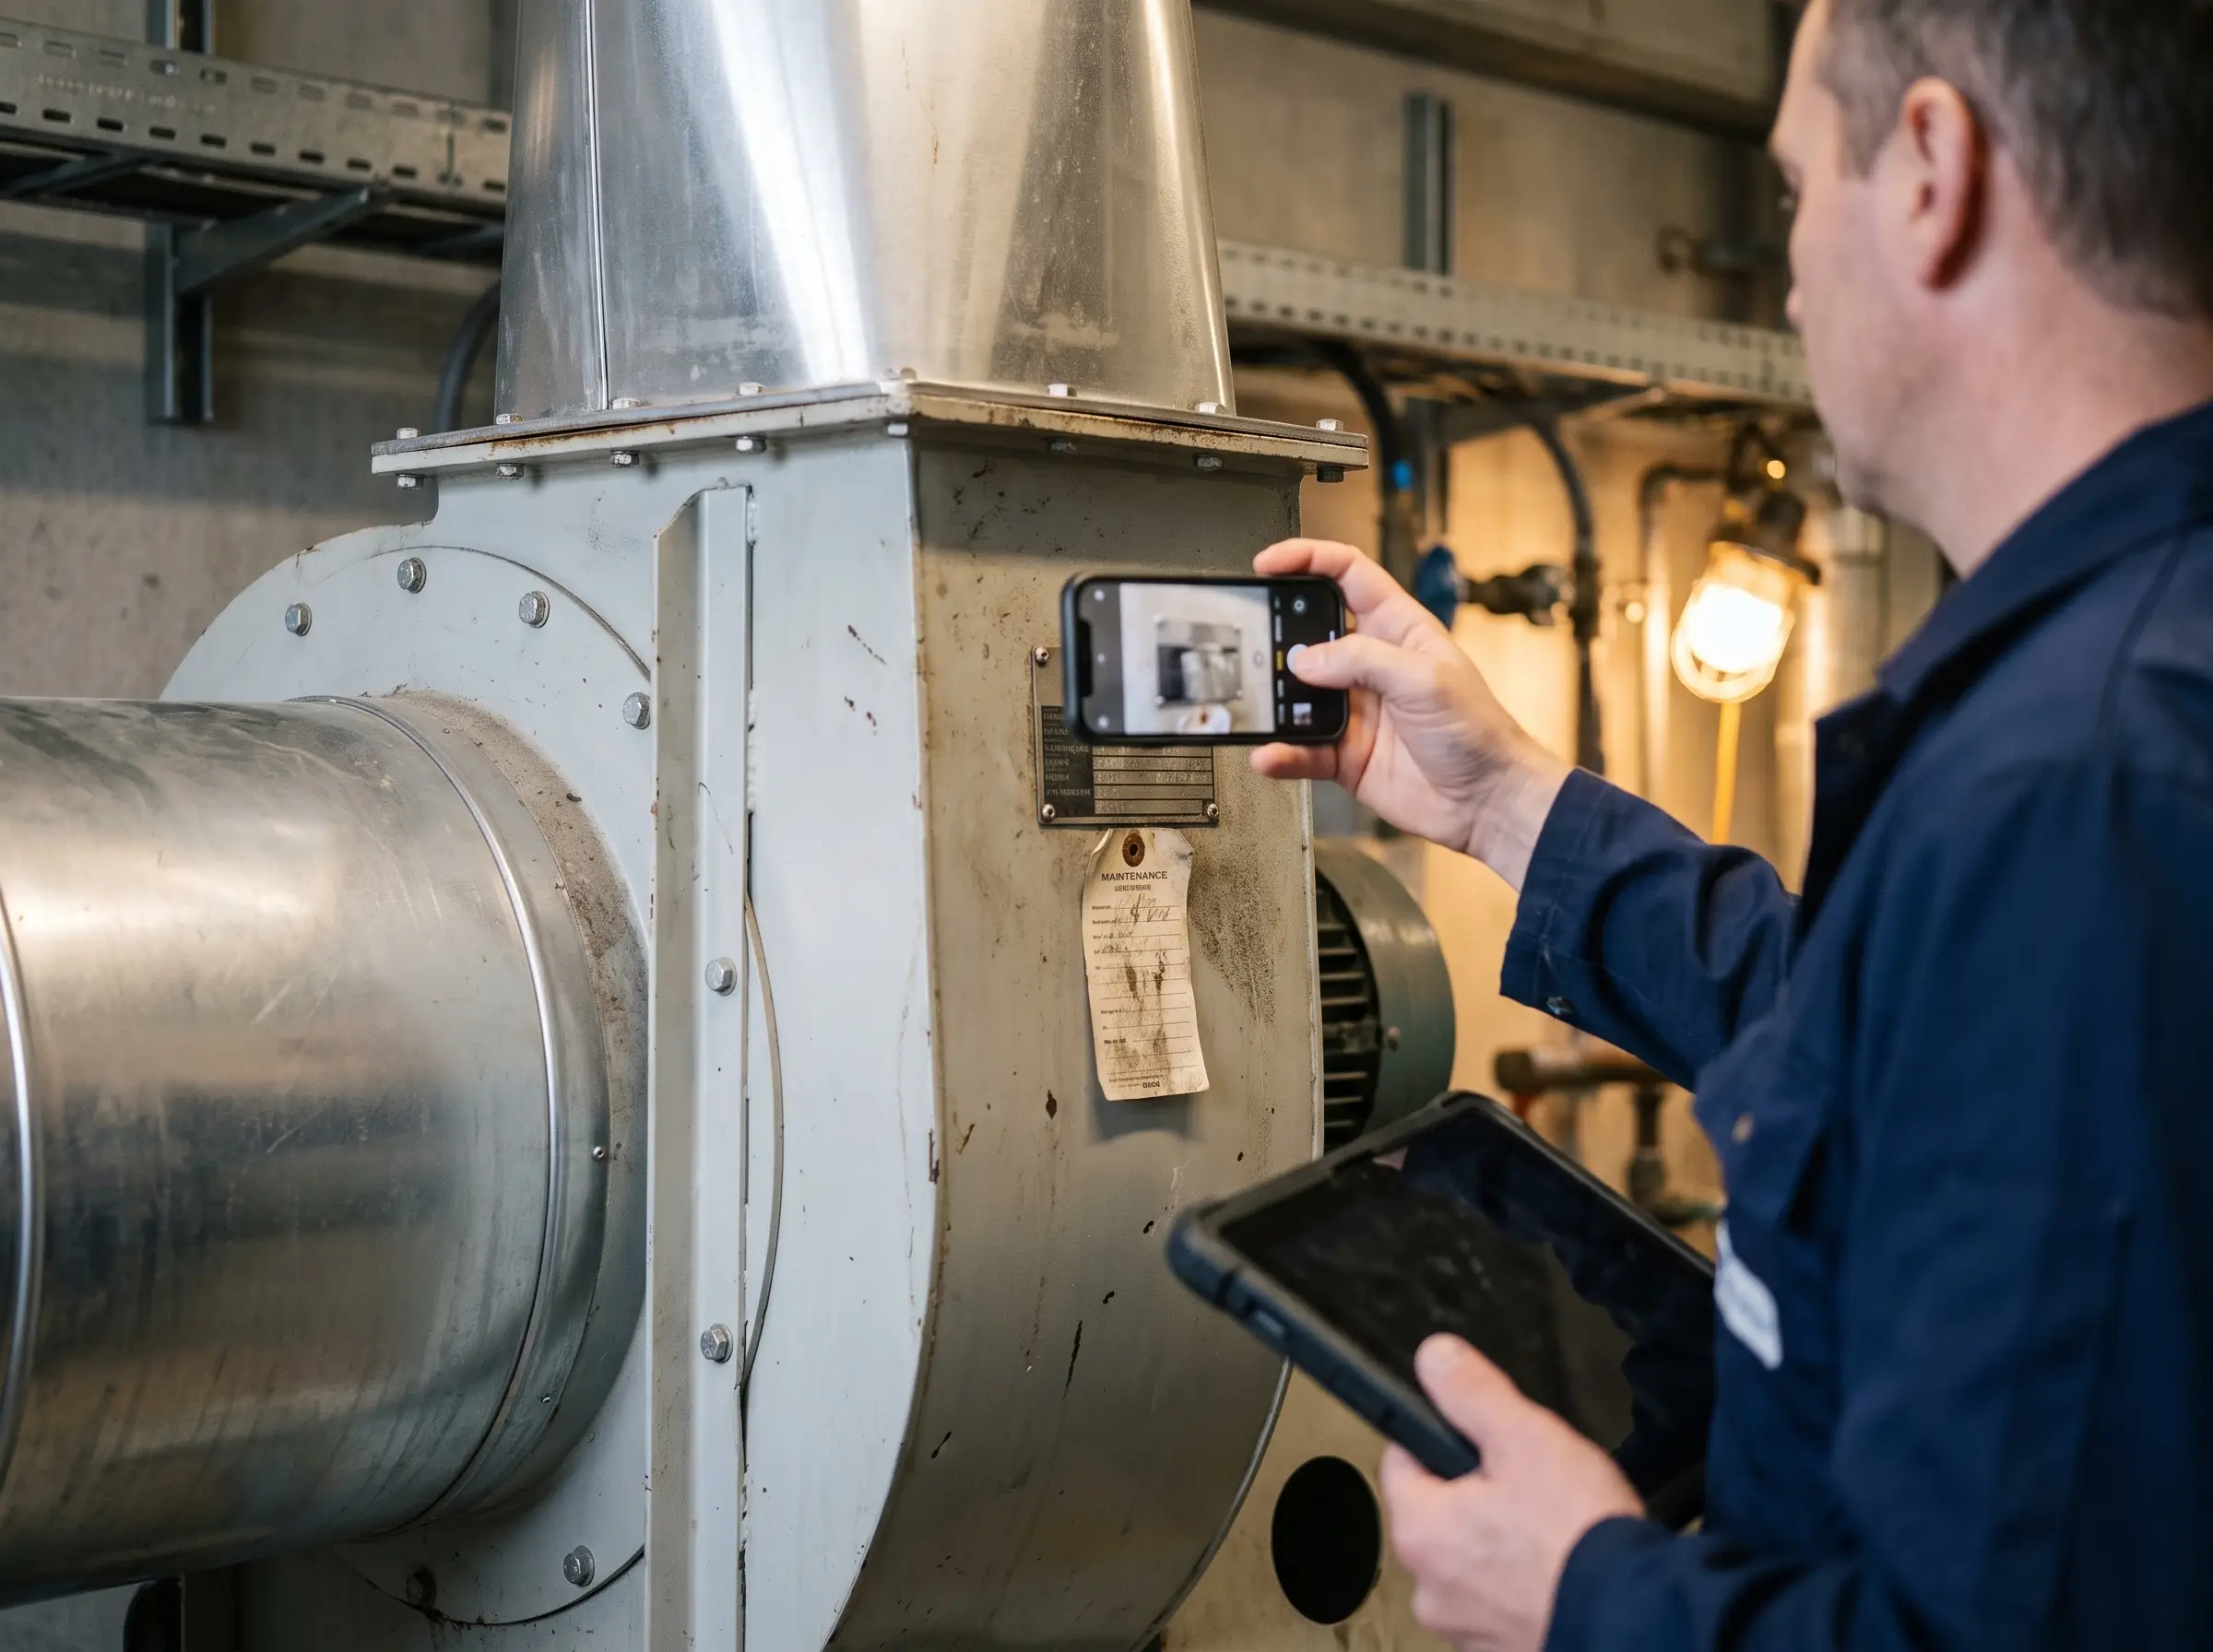
Request an Assessment with a short description of the exhaust source and the heating demand you would like to offset. Photos and equipment information are helpful but optional for the first conversation.

Facility manager photographing exhaust equipment for an opportunity screen
START SMALL

What happens next

A first conversation helps ThermStar understand the operating goal, the facility context, and the people involved in the decision. 

From there, the team can identify the smallest useful information request and determine whether a screen, technical review, partner discussion, or document request is appropriate.

This approach keeps the process proportionate to the opportunity while giving operations, finance, engineering, health and safety, and sustainability stakeholders clear information for the next decision.

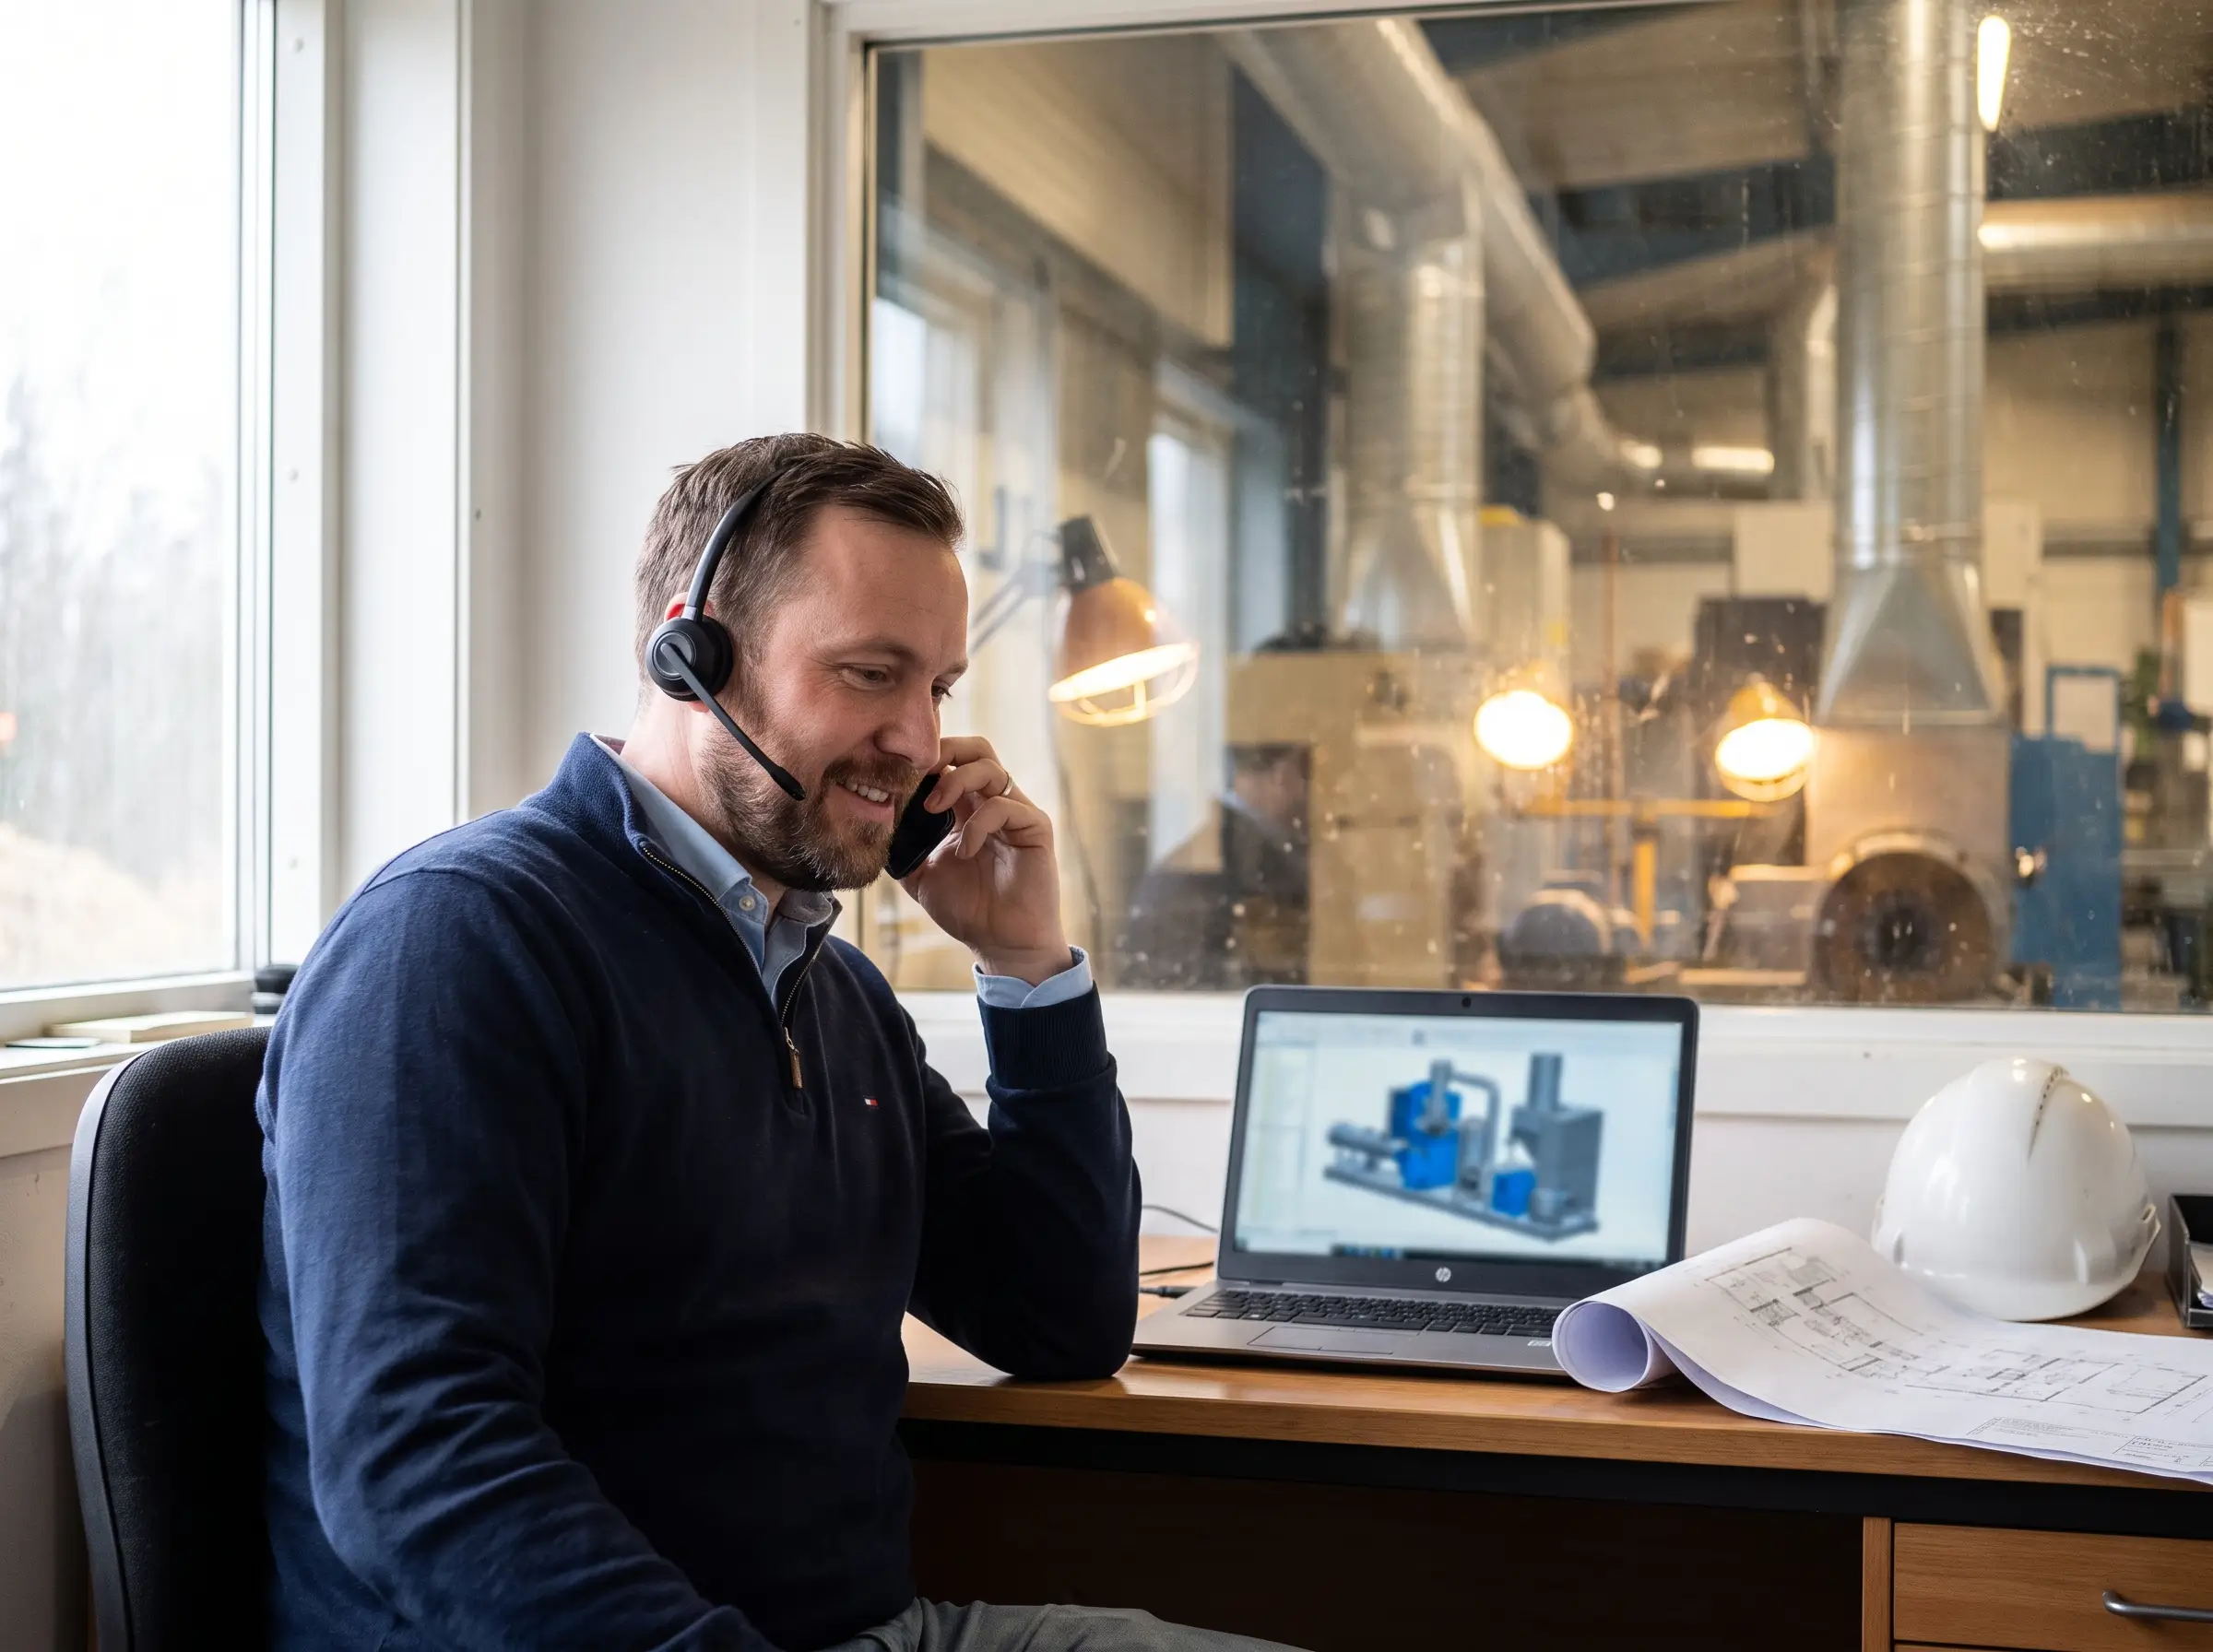
Engineer on the phone at a desk with plans and a laptop
COMMON QUESTIONS

What to know before you start

What makes a food processing heat recovery project viable

The strongest candidates have a consistent thermal source, a productive receiving load, useful temperature alignment, overlapping operating hours, workable integration, and enough displaced energy value to support the project. A high exhaust temperature by itself is not sufficient.

Possible uses include approved process air, makeup air, process water, domestic hot water, boiler feedwater, and other thermal demands. The selected use must be compatible with the available temperature, capacity, schedule, location, controls, and facility requirements.

Yes. An organization can begin with a portfolio screen using consistent information from multiple sites. ThermStar can help identify which locations deserve deeper review. Findings from one project may inform later work, but each facility still requires confirmation.

Savings are based on useful recovered energy and the energy it displaces. A project specific method may use temperature, fluid flow, operating time, equipment status, baseline efficiency, and approved conversion factors. Actual reporting depends on the installed monitoring and any utility or internal requirements.